What Are Good Manufacturing Practices Definition (GMP)?
Good Manufacturing Practices (GMP) are the practices and conditions used to help ensure that products are manufactured safely, consistently, and under controlled conditions.
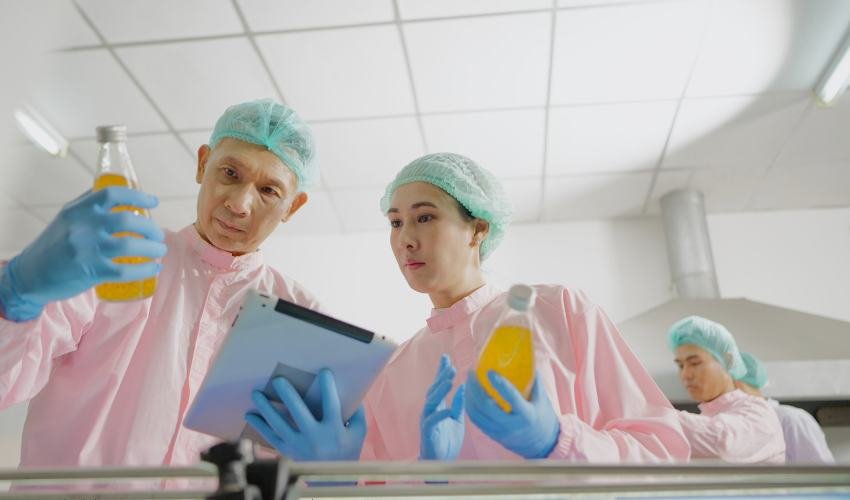
In the food industry, GMP provides a foundation for controlling contamination risks through areas such as sanitation, personnel hygiene, facility maintenance, equipment, storage, supplier controls, and documented procedures.
This guide explains the Good Manufacturing Practices definition, why GMP matters, how GMP supports food safety systems, and how Canadian food businesses can implement effective GMP controls.
What Is the Definition of Good Manufacturing Practices?
Good Manufacturing Practices (GMP) are a set of regulations, codes, and guidelines for the manufacturing of food, pharmaceuticals, cosmetics, and other products. These practices ensure that products are consistently produced and controlled in accordance with quality standards.
In short, GMP is a set of principles that guide how products are made to minimize risks involved in production, especially risks that cannot be eliminated through testing the final product alone.
GMP ensures product quality, consumer safety, and regulatory compliance. Health and regulatory authorities worldwide enforce these practices.
Why Are Good Manufacturing Practices Important?
GMP requirements vary depending on the industry, product, activity, and jurisdiction. In Canadian food operations, GMP principles are reflected in preventive food safety requirements and provide important foundational controls for sanitation, hygiene, facilities, equipment, storage, and other food safety practices.
Here’s why GMP is vital:
Protects Consumer Health
Definition of Good Manufacturing Practices plays a pivotal role in protecting consumer health. By minimizing contamination, mix-ups, and errors, it ensures that only safe, high-quality products reach consumers, thereby instilling trust and reassurance.
Ensures Product Consistency
Every batch must meet the same standards. GMPhelps standardize procedures to guarantee quality in every production run.
Regulatory Compliance
Failure to follow Good manufacturing practices can result in severe penalties, product recalls, or facility shutdowns, significantly impacting a business’s reputation and financial stability.
Builds Brand Reputation
Compliance with the Definition of Good Manufacturing Practices not only boosts trust among consumers, partners, and regulators but also positions your brand as reliable and responsible, which can lead to increased customer loyalty and market share.
Reduces Waste and Operational Costs
By catching errors early and preventing rework or recalls, GMP saves time and money. For instance, by ensuring consistent product quality, GMP can reduce the need for product rework, thereby saving on production costs and resources.
While GMPprograms vary by industry and jurisdiction, the core elements remain consistent:
Personnel and Hygiene
Only qualified, trained individuals should be involved in production. Personnel hygiene and clear roles are emphasized.
Premises and Equipment
Facilities must be appropriately designed, well-ventilated, and maintained. Equipment should be cleaned and calibrated regularly.
Cleaning and Sanitation
Cleanliness must be maintained across facilities, equipment, and employee practices. Cross-contamination is strictly avoided.
Raw Materials and Supplier Controls
All ingredients or materials must meet quality standards, and reliable supplier verification is necessary.
Production and Process Controls
All operations should follow documented procedures. Any deviation must be investigated and corrected.
Documentation and Record-Keeping
Complete and accurate records provide objective evidence that required activities were performed and verified.
Maintenance and Calibration
Processes must be validated to produce consistent outcomes, and verification activities must confirm compliance.
Implementing GMP in Your Organization
Here’s how businesses can effectively adopt GMP:
Start with a Gap Assessment
Identify where current operations fall short of GMP requirements.
Develop GMP Procedures and Programs
Develop or revise SOPs, sanitation programs, personnel-hygiene procedures, maintenance controls, supplier controls, monitoring procedures, and documentation systems.
Train All Staff
Ensure employees receive GMP training appropriate to their responsibilities and understand the procedures relevant to their work.
Maintain Records
Create a system for tracking quality checks, batch logs, sanitation reports, and training records.
Conduct Internal Audits
Regular audits help ensure ongoing compliance and highlight areas for improvement.
Certification or Customer Requirements, Where Applicable
Some customers, markets, or certification programs may require evidence of GMP implementation or specific certification. Requirements vary by industry and certification scheme.
GMP and HACCP: How They Work Together
GMP and HACCP serve different but complementary purposes.
GMP establishes the basic operational and hygienic conditions needed to produce food safely.
HACCP systematically identifies and controls significant food safety hazards associated with the product and process.
Together, GMP, prerequisite programs and HACCP provide a stronger food safety framework.
Whether you’re building your first GMP system or upgrading your existing one, we can help you achieve full compliance and operational excellence.
Conclusion
Good Manufacturing Practices provide the practical foundation for producing food safely and consistently. For Canadian food businesses, effective GMP controls help manage sanitation, personnel hygiene, facilities, equipment, storage, supplier controls, documentation, and other preventive food safety conditions.
GMP is most effective when it is implemented as part of the broader food safety system rather than treated as a standalone checklist.
Need help developing or improving your GMP program? Arnika provides GMP consulting, auditing, training, and certification-readiness support across Canada.
Frequently Asked Questions (FAQs)
What is the definition of GMP in simple terms?
GMP, or Good Manufacturing Practices, are the practices and conditions used to help ensure products are manufactured safely, consistently, and under controlled conditions.
Is GMP mandatory in Canada?
GMP requirements depend on the industry, product, activity, and applicable regulations. For Canadian food businesses, GMP principles form part of the broader preventive food safety framework and help control conditions such as sanitation, hygiene, facilities, equipment, storage, and contamination prevention.
What’s the difference between GMP and HACCP?
GMP provides foundational operational and hygiene controls, while HACCP is a systematic approach for identifying and controlling significant food safety hazards. GMP and prerequisite programs support the effective implementation of HACCP.
Is GMP certification required?
There is no single universal GMP certification that applies to every Canadian food business. Certification requirements depend on the applicable customer, market, certification programme, or industry. Arnika can help businesses assess requirements and prepare their GMP system for applicable audits or certification.
Who should receive GMP training?
Employees should receive GMP training appropriate to their responsibilities. This can include production, sanitation, quality, warehouse, maintenance, supervision, and management personnel whose work affects food safety or product quality.